Reduce AAC block breakage during separation and packing by identifying the first damaging contact, checking the condition of the blocks entering the station, and validating the handling setup for the actual product. Follow marked batches through separation, transfer, stacking, and strapping. Increasing clamping force or adding tighter straps without that evidence can move the problem to another point in the process.
The workflow below is a practical investigation and purchasing guide for AAC factories. It does not prescribe a universal hydraulic pressure, separation stroke, stack height, or strap tension; those limits depend on the equipment, product, packaging design, and approved operating procedure.
Where Should Breakage Be Counted?
Count damage at defined handover points so that each station receives an observable starting condition. Inspect representative material before separation, after separation, after transfer, and after packing. Recording only rejects at the end cannot reveal which operation introduced the damage.
Use a consistent definition of a rejected block and distinguish a missing corner, a surface mark, and a through-crack. The customer’s product specification should determine acceptance. Photographs help operators apply that definition consistently across shifts.
- Record batch identity and product dimensions.
- Count the units inspected at each observation point.
- Record new defects separately from damage already present.
- Keep the reason for rejection beside the count.
- Note any stop, restart, or manual intervention during the sample.
For related problems elsewhere in the line, use the overview of AAC machine faults and production symptoms. Localize the loss before deciding which section needs corrective work. This avoids assigning every damaged finished block to the last machine that handled it.
What Must Be Checked Before Changing the Separator?
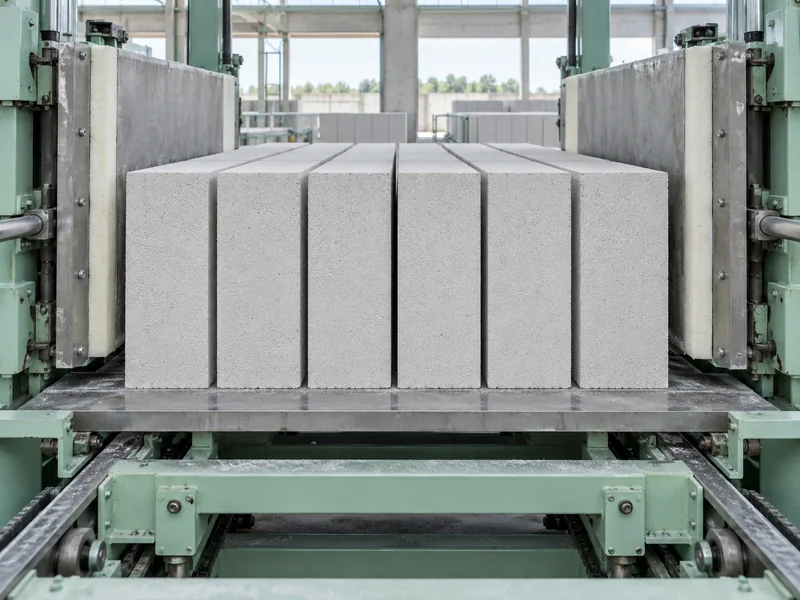
Confirm the incoming product, its orientation, and the intended separation process against the installed machine documentation. Plants can use different layouts and separation arrangements. A setting from another installation is not a reliable starting point unless the relevant conditions are equivalent.
Observe whether the blocks arrive consistently positioned and whether existing damage is visible. Check the planned product sizes against the equipment’s approved working range. If incoming material is outside its release criteria, hold it for investigation rather than relying on the separator to correct it.
Why Does the Separation Arrangement Matter?
The equipment review must identify what is being separated, at which production stage, and how the load is supported. Draw the actual flow from the preceding station to the next transfer. That simple drawing makes assumptions about orientation, support, and product condition easier to challenge.
Runding’s AAC separator page describes adjustable clamping and separation movements. Ask the supplier to confirm the configuration and operating sequence intended for the specific project. Verify performance with representative products instead of treating every published feature as a universal setting.
How Can Contact Marks Guide a Clamp Inspection?
Map marks against the actual contact surfaces and compare them with an accepted run. A mark at a clamp location is a useful lead, but inspection must establish whether the contact geometry, positioning, pad condition, or another factor is responsible. Do not diagnose pressure from a photograph alone.
| Observation | Investigation Priority | Evidence to Keep |
| Damage matches one contact location | Inspect that surface and compare the opposite side | Contact map and component condition |
| The group moves during pickup | Review positioning and the approved gripping sequence | Safe observation of the complete cycle |
| Damage appears on release | Check support and landing alignment | Before-and-after release images |
| Only one product size is affected | Verify the selected product setup and working range | Product recipe and dimension records |
Inspect contact components only with the required isolation and access controls in place. Replace or repair them according to the equipment procedure, then verify the result. Record component changes so a later improvement can be linked to actual work.
How Should Transfer and Landing Be Assessed?
Observe the entire transfer, including pickup, travel, deceleration, landing, and release. A smooth travel section does not establish that the final handover is satisfactory. Concentrate on where the load changes support or where separate machines must coordinate.
Runding’s AAC block grabber is intended for lifting and transferring block groups. During selection, define the real bundle geometry, weight range, travel path, and receiving surface. Confirm those requirements with the supplier for the proposed machine rather than choosing by nominal lifting capacity alone.
- Check whether the group arrives in the intended position.
- Verify that the receiving support matches the approved arrangement.
- Observe whether loose pieces or contamination interfere with seating.
- Review synchronization at the interface with the next conveyor or platform.
- Inspect the product immediately after the handover.
Production interruptions deserve their own observation. A restart may present a different queue or load position from steady running. Include that condition in commissioning and operator training.
What Should Be Verified Before Strapping?
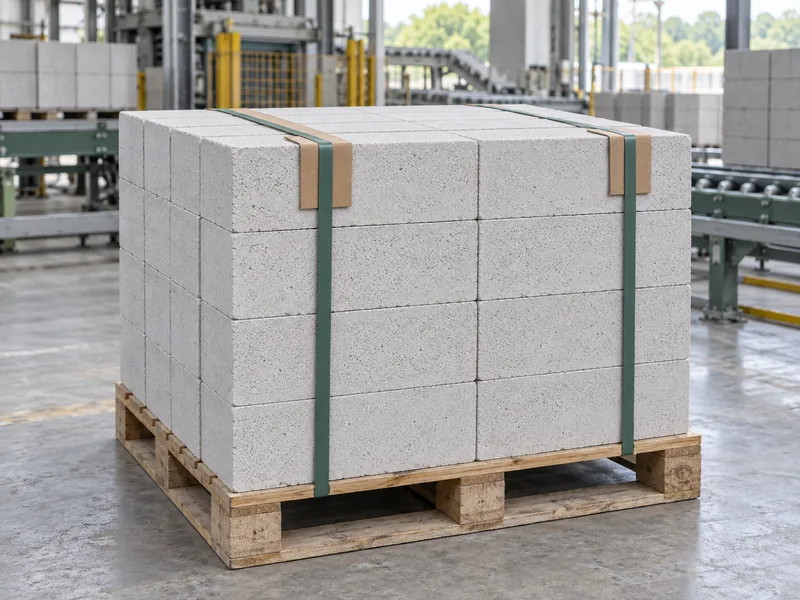
Verify that the stack and its support satisfy the approved packaging arrangement before applying straps. Strapping should secure an accepted bundle; it should not be used to pull a visibly misaligned stack into shape. Isolate the source of any poor alignment first.
Check the pallet or other support for condition, suitability, and contact with the load. Record the approved stacking pattern and edge protection arrangement for each product family. When the package design changes, treat it as a controlled change with its own acceptance check.
How Should Strap Settings Be Validated?
Use the packaging supplier’s and equipment manufacturer’s procedure for the selected strap, bundle, and protection materials. Inspect the package after application and after the defined handling trial. A visually tight strap is not a measurement of an acceptable package.
Record strap location, protective materials, and the equipment setup used during the trial. If marks or damage appear, preserve their location and timing before adjusting the system. For the packing trial, document the approved adjustment before running the next sample, and postpone other adjustments until the team has compared the resulting strap contact marks and package condition.
ASTM C1691 includes shipping and handling within its scope for unreinforced AAC masonry units. Use the applicable product and transport requirements when establishing the factory’s acceptance plan. The existence of a standard does not mean a particular package has been tested or certified.
How Can a Trial Separate Product Issues from Handling Issues?
Compare identified, accepted incoming material under a documented handling configuration. Keep a record of its condition before each operation and inspect it immediately afterward. Where comparison conditions differ, state the limitation instead of calling the result conclusive.
For example, a hypothetical trial might find clean edges after separation and a recurring mark only after landing on one platform. The next investigation would focus on that handover. It would be premature to change the AAC formulation based solely on the final reject count.
- Select representative product sizes and define the inspection sample.
- Confirm incoming acceptance and document the initial condition.
- Run the approved baseline setup.
- Record defects at each handover.
- Investigate the first operation associated with new damage.
- Repeat the relevant comparison after an authorized correction.
If incoming quality is inconsistent, the trial must acknowledge that uncertainty. The discussion of raw material fineness and AAC quality provides one related upstream topic. Use process records and testing to decide whether upstream investigation is warranted.
What Should Buyers Ask During an Acceptance Demonstration?
Ask for a demonstration based on the intended products and interfaces, with agreed records of quality and throughput. Include the least convenient product configuration within the agreed supply scope. A favorable run of one easy size does not establish performance across the required range.
- Which product sizes and bundle weights are included in the demonstration?
- How will incoming defects be distinguished from newly introduced damage?
- What happens after a stopped or interrupted cycle?
- How are changeovers checked before production resumes?
- Which maintenance tasks affect contact geometry and positioning?
Use the article on AAC production capacity bottlenecks when evaluating the wider line. A packing upgrade should be assessed against the actual upstream supply and downstream dispatch arrangement. Compare usable output and maintenance demands alongside advertised cycle speed.
How Should Improvements Be Kept in Daily Production?
Turn the successful trial configuration into a controlled operating record, then verify it at changeover and restart. Keep the relevant contact inspection and cleaning tasks in routine maintenance. Review any return of the same defect against the recorded baseline.
The most useful breakage report identifies where damage begins and what changed before it returned. With that information, production and maintenance can choose a focused correction. Consistent product handovers make the improvement repeatable after the commissioning team has left.