Buyers should use an AAC equipment factory visit to verify manufacturing capability and an operating reference plant visit to verify how a comparable production system performs in daily use. The strongest evidence combines direct observation, traceable records, product checks, and conversations with the people who operate and maintain the line. A polished tour or one successful production cycle cannot answer all four questions.
Prepare a visit brief before travel and record findings as observed, documented, reported, or still unverified. This keeps the purchasing team from treating a supplier explanation as a completed inspection. The visit should reduce uncertainty about the proposed equipment, not merely confirm that a factory exists.
Before Departure: Is This the Right Site to Inspect?
Match the destination to the purchasing uncertainty you want to resolve. Visit the assembly workshop for evidence about fabrication and pre-shipment inspection; visit a running customer installation for evidence about staffing, machine coordination, and routine upkeep. Some projects need both visits because neither location provides the complete picture.
Ask how the reference installation compares with your project in raw materials, product sizes, automation, climate, and operating schedule. A successful line producing a different product mix is useful evidence of experience, but it does not automatically validate your output assumptions. List these differences explicitly.
- Confirm whether the proposed machine generation will be available to view.
- Arrange access during a scheduled customer production shift so the team can observe ordinary interruptions and material transfers.
- Agree on permitted photography, sampling, and access to non-confidential records.
- Arrange time with production, maintenance, and quality personnel.
- Send the unresolved quotation questions in advance so relevant evidence is ready.
Bring someone who understands production interfaces as well as purchasing. For a substantial project, a suitably qualified independent inspector can help evaluate technical evidence. Define the inspection scope and limitations instead of expecting a short visit to replace design review or formal acceptance.
At the Equipment Factory: Can the Supplier Prove How It Builds?
Follow one component from identification through manufacture, inspection, and assembly. The aim is to understand whether quality records correspond to the actual item and whether problems are detected before shipment. A room full of machines proves available assets, but not necessarily a controlled manufacturing process.
Can Drawings, Components, and Inspection Records Be Connected?
Ask the host to select an accessible component and show its current drawing revision, material identification where applicable, and inspection result. Check whether the record identifies the component and the instrument used. If a tolerance matters to alignment or product quality, ask how that feature is measured.
Observe machining surfaces, assembly fit, cable routing, protective covers, and access for future service. Avoid judging structural adequacy or weld integrity solely from appearance. Those questions may require engineering documentation and inspection by qualified personnel.
Which Assemblies Come From the Workshop or Its Subcontractors?
Identify which assemblies the supplier manufactures, which it buys, and how purchased items are checked. Outsourcing is not inherently a weakness; unclear responsibility is. Ask who handles a defect involving a purchased drive, sensor, control component, or other critical part.
Compare the machines being assembled with the specified AAC equipment and process sections in your proposal. Record visible differences and ask whether they are customer-specific options or changes to the standard design. Ask the host to identify the displayed machines that correspond to your equipment schedule, including any accessories priced separately.
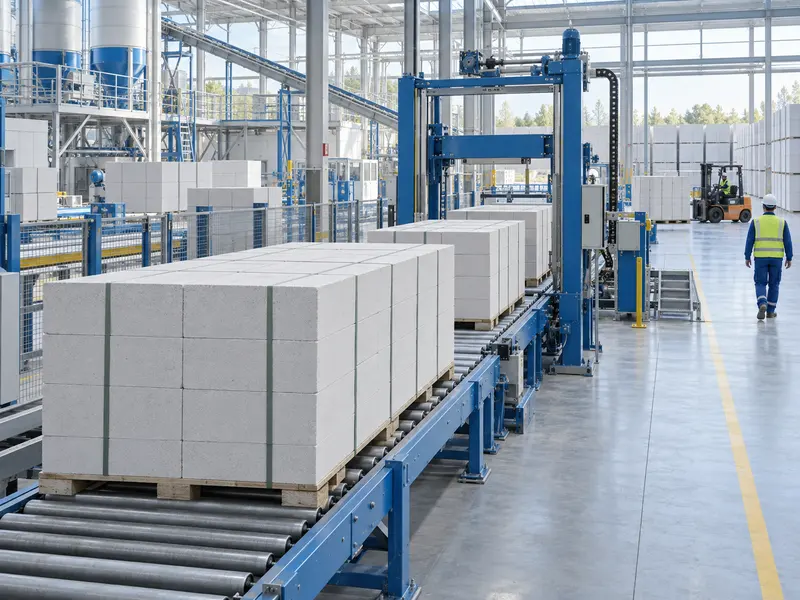
At the Reference Plant: What Happens During an Ordinary Shift?
Walk the material route with the operator and watch the transitions between machines. A machine may cycle quickly while the overall line waits for a mould, transfer unit, autoclave slot, or packing station. Note queues, interruptions, manual interventions, and recovery time.
Ask for records covering a representative operating period and clarify what the figures count. Separate produced volume, accepted volume, dispatched volume, and paid sales. Keep a separate column for each volume measure so dispatch totals do not become a substitute for quality-accepted output.
| Observation | Record That Helps Verify It | Question to Ask |
| Regular line movement | Shift output and downtime logs | Which interruptions recur most often? |
| Consistent finished blocks | Batch-linked quality results | How are rejected products recorded? |
| Manageable maintenance | Work orders and spare-part usage | Which repairs need outside support? |
| Stable staffing | Shift role list | Who covers breaks, faults, and cleaning? |
| Orderly dispatch | Damage and customer complaint records | Where does handling damage appear? |
Ask the operator to describe a recent interruption, its cause, and the recovery steps. A realistic account is often more informative than a claim that failures never occur. Cross-check the explanation against the maintenance or shift record when the host permits access.
Observe fault recovery without asking anyone to create a hazardous condition. Never request bypassing an interlock or opening a protected operating area for a better photograph. Demonstrations involving safety functions should follow the plant’s approved procedure and be conducted by authorized personnel.
At the Quality Station: What Do the Products Actually Show?
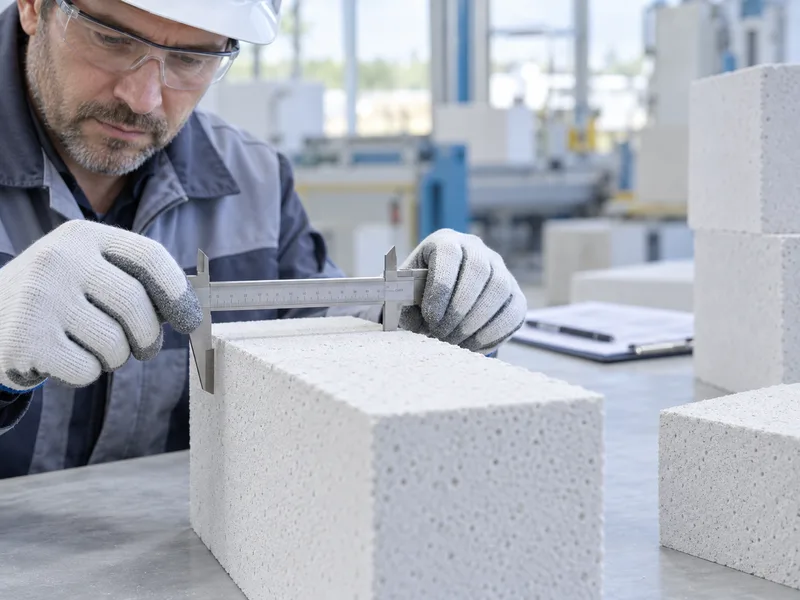
Inspect products from identifiable batches rather than selecting only display samples. Look at dimensions, chipped edges, cutting marks, separation damage, and consistency across the sample set. Visual checks can reveal handling issues, but strength and other declared properties require the appropriate tests.
Agree on a sampling method with the host and record the product type, batch reference, and measuring method. A few blocks cannot establish long-term process capability. They can, however, show whether the plant has a repeatable way to identify and investigate defects.
- Check whether measurements are recorded against defined product requirements.
- Ask how measuring equipment is checked or calibrated.
- Confirm how nonconforming material is segregated and dispositioned.
- Compare samples before and after packing where access permits.
- Request an explanation of unusual defects rather than guessing their cause.
The discussion of AAC cutting marks and edge damage can help organize the questions, particularly when separating process defects from later handling damage. Use the visit to establish what evidence the supplier can provide for your intended product range.
In the Maintenance Area: Could Your Team Keep This Line Running?
Check service access, replaceable wear parts, diagnostic information, and the skills needed to recover from faults. A technically capable plant may still be a poor fit if your maintenance team cannot obtain parts or support promptly. Discuss local capability honestly.
Ask to see how an operator identifies an alarm and finds the corresponding instructions. Review whether manuals, electrical drawings, spare-part lists, and software backups are supplied in a usable language and format. Confirm who controls access to backups and what assistance is available after handover.
For important wear items, request part identification, expected inspection practices, and replacement lead-time information. The AAC spare-parts planning guide helps distinguish a sensible startup stock from a large but poorly targeted spare package. Actual quantities should follow the installed equipment and supply conditions.
After the Visit: Which Findings Change the Buying Decision?
Before leaving the site, assemble the inspection notes into an evidence register. For every open purchasing question, attach the relevant observation or permitted document, identify the missing proof, and name the person who will obtain it. Label photographs with their actual location so later reviewers understand what they depict.
Separate a satisfactory observation from a contractual commitment. If the reference plant uses additional equipment or staffing to achieve its result, establish whether your proposal includes the same resources. If a concern requires a trial, define that trial before treating the issue as resolved.
- Close factual discrepancies between the quotation and the equipment inspected.
- Request missing records with clear due dates.
- Revise the project assumptions where reference conditions differ.
- Carry unresolved performance questions into the acceptance procedure.
- Document why the evidence supports proceeding, modifying the scope, or delaying selection.
Judge the visit by the purchasing uncertainties it resolves. A documented account of ordinary operation, maintenance demands, and outstanding technical questions is more useful than a collection of favorable impressions. Use that account to revise the equipment scope before placing the order.