AAC batching accuracy depends on the material that reaches the mixer, not simply the number displayed when a feeder stops. Check the approved recipe, the weighing system, the feeding sequence, and the complete discharge as one connected process. For slurry, also establish whether the recipe refers to wet mass, dry solids, or another defined basis.
A useful investigation follows one identified batch from its source containers into the mould. This makes it possible to separate measurement error from delivery loss and composition variation. The checks below form an investigation plan; equipment adjustments and acceptance limits must follow the plant’s validated procedures.
Start With Three Different Quantities
The recipe target is the quantity requested, the scale result is the quantity indicated, and the delivered quantity is what actually enters the next process. These can disagree for different reasons. Treating all three as a single figure hides the point at which control was lost.
- Requested: the approved ingredient target for the selected product and batch size.
- Indicated: the settled weighing result, with its units, tare condition, and measurement uncertainty.
- Transferred: the material discharged through the intended route, accounting for retained material or an interrupted transfer.
Before investigating a mechanical fault, confirm that everyone is comparing the same batch and ingredient. A production screen may show a current target while an exported report contains a previous result. Recipe version, equipment identity, and timestamps make that distinction visible.
Follow One Batch Through Four Checkpoints
Checkpoint One: Recipe and Material Identity
Confirm the selected recipe version, product density class, batch size, ingredient names, and units. Check whether an operator correction was authorized and recorded. A correctly functioning scale can still execute the wrong instruction.
For slurry, a stable wet mass does not establish a stable solids contribution. Review representative concentration measurements and the plant’s approved method for converting them into dosing instructions. The guide to slurry storage and consistent feed explains why sampling location and withdrawal history matter.
Keep raw material changes visible in the batch record. A delivery change, a different holding period, or a revised dilution practice can explain why yesterday’s settings no longer produce the same behavior. Do not compensate for an unidentified change by quietly editing several ingredient targets.
Checkpoint Two: The Weighing Assembly
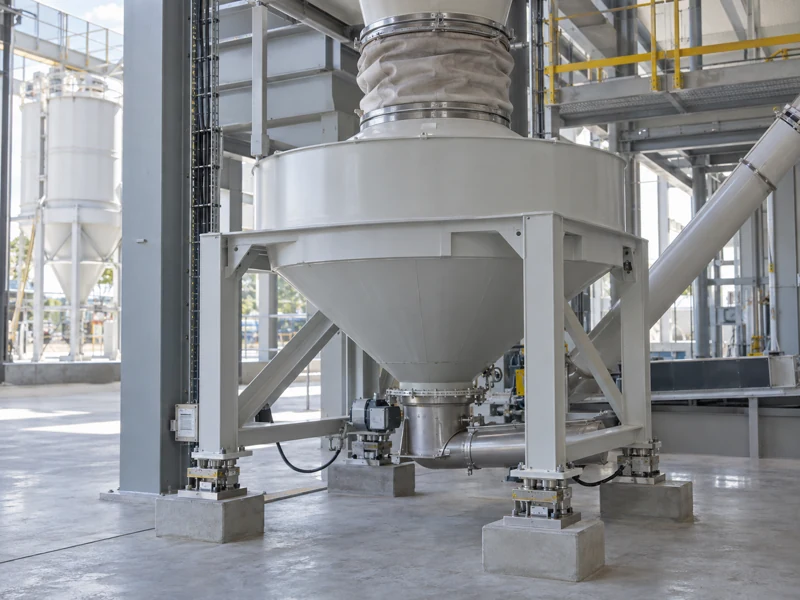
Review the condition of the complete weighing assembly with the maintenance and instrumentation team. Material buildup, an unintended mechanical contact, or a rigid connection can create forces that are not part of the intended load. Establish safe access before inspecting supports, flexible connections, or the discharge mechanism.
Record the empty indication before filling and after discharge under comparable conditions. An unexplained difference is a reason to investigate residual material, mechanical restraint, or measurement drift. Repeatedly pressing zero can conceal the pattern that would help locate the cause.
NIST’s explanation of measurement traceability emphasizes documented calibration chains and measurement uncertainty, while noting that traceability alone does not establish fitness for purpose. Apply that distinction when reviewing a scale certificate: the reference, range, uncertainty, and actual process requirement all matter. A certificate is one part of the evidence for a suitable measurement system.
Checkpoint Three: Feeding and Cutoff
Compare the indication when feeding stops with the settled result after material in transit has arrived. The difference can reveal delivery that continues beyond the stop command. Use the system’s approved records or a controlled observation rather than assuming the feeder and weighing display respond at the same instant.
Look for patterns across comparable batches: consistent overshoot, irregular jumps, or a change associated with source level. These patterns support different investigations. Any alteration to coarse feeding, fine feeding, or cutoff compensation should be documented and evaluated within the manufacturer’s control strategy.
The site’s batching and pouring equipment should be considered as a coordinated section when defining that investigation. The practical question is how the selected feeder, weighing arrangement, controls, and downstream receiver work together. A quoted component accuracy does not describe every operating condition of the installed system.
Checkpoint Four: Discharge and Receipt
Observe whether discharge completes within the expected sequence and whether the receiving stage is ready. A blocked route, a retained pocket of material, or an interrupted cycle can separate the weighing result from the amount actually received. Record the exception instead of treating the batch as normal because the weighing target was reached.
Small additions deserve their own verification method. Where an aluminum slurry mixing machine prepares the addition, preparation consistency and the subsequent dosing sequence are separate checks. Follow the approved handling procedure and do not improvise changes to concentration or addition quantity during a weighing investigation.
Choose the Test From the Observed Pattern
| Observed Pattern | Useful Comparison | What It Can Clarify |
| Empty indication changes after discharge | Before and after readings with residual material observations | Retention, restraint, or measurement drift |
| Settled result exceeds the stop indication | Feeder stop time and final stable reading | Material arriving after cutoff |
| Wet slurry mass repeats but production varies | Representative concentration and batch history | Composition variation despite repeated mass |
| Weighing passes but the receiver reports a shortage | Discharge completion and transfer exceptions | Loss between weighing and receipt |
This table identifies comparisons, not automatic diagnoses. More than one cause can produce the same symptom, and two faults may coexist. Preserve the original readings before changing the system so that the team can evaluate the effect of each correction.
A Small Arithmetic Example With an Important Boundary
Consider an illustrative recipe requiring 600 kg of slurry solids. At a measured solids mass fraction of 60%, the corresponding wet slurry mass is 1,000 kg; at 55%, it is approximately 1,091 kg. The calculation is dry solids divided by the solids mass fraction.
This example is not a recommended recipe adjustment. Changing wet slurry mass also changes the water introduced, and the complete formulation must remain within the approved process design. It demonstrates why checking only the wet weighing result can miss a material balance change.
Keep the laboratory result and its sampling details beside the calculation. A precise calculation using an unrepresentative sample still produces an unreliable instruction. The article on raw material fineness and AAC expansion provides additional context for material changes that weighing alone cannot resolve.
Keep Verification Separate From Adjustment
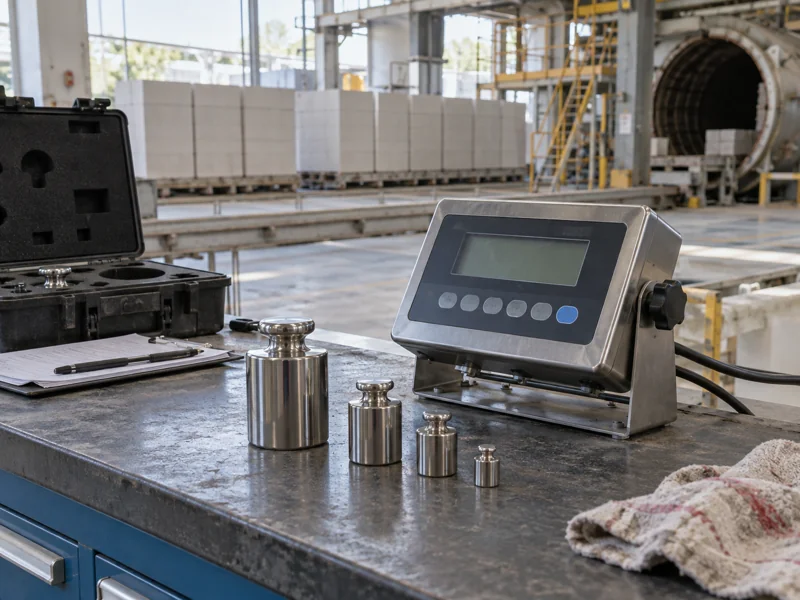
A verification asks whether the installed system meets an agreed requirement; an adjustment changes its response. Record which activity took place, who performed it, and which procedure was used. Otherwise, a later reviewer may interpret a corrected reading as evidence that the original condition was acceptable.
Ask the responsible specialist to select reference loads and test points appropriate to the operating range and access arrangements. A satisfactory check near one load does not, by itself, describe performance at every batch size. Include repeatability and the effect of ordinary operating conditions in the verification plan where relevant.
When a check fails, identify potentially affected batches using the last satisfactory evidence and the available operating history. Production and quality staff should decide the disposition of those batches through the established quality procedure. Do not erase the original event by replacing its recorded result with a later successful test.
After maintenance, retain the before and after findings and confirm the required release checks. This gives the next shift a reason to trust the system and a clear record of what changed. It also avoids repeating an investigation simply because the evidence was left in a technician’s notebook.
Close the Investigation With a Repeatable Batch Audit
Select a manageable series of comparable batches and record the same fields each time. Include successful batches as well as exceptions, because normal behavior provides the reference for interpreting a fault. Avoid selecting only the most dramatic event.
- Record recipe version, material identity, batch size, and equipment number.
- Capture empty, cutoff, and settled indications with units and timestamps.
- Confirm discharge completion and identify any material held or diverted.
- Attach applicable concentration results and sampling details.
- Record the single approved intervention and compare subsequent batches.
Agree on the acceptance method before declaring the issue resolved. The result should show that the relevant quantity is controlled under representative operating conditions, with exceptions handled consistently. An improvement in one displayed number is not enough if transfer failures remain unexplained.
When asking Runding to review a dosing concern, provide this batch record alongside equipment identification and the current operating sequence. The broader AAC machine troubleshooting guide can help connect the finding to downstream symptoms. A clear measurement chain gives both plant staff and the supplier a practical starting point for correction.